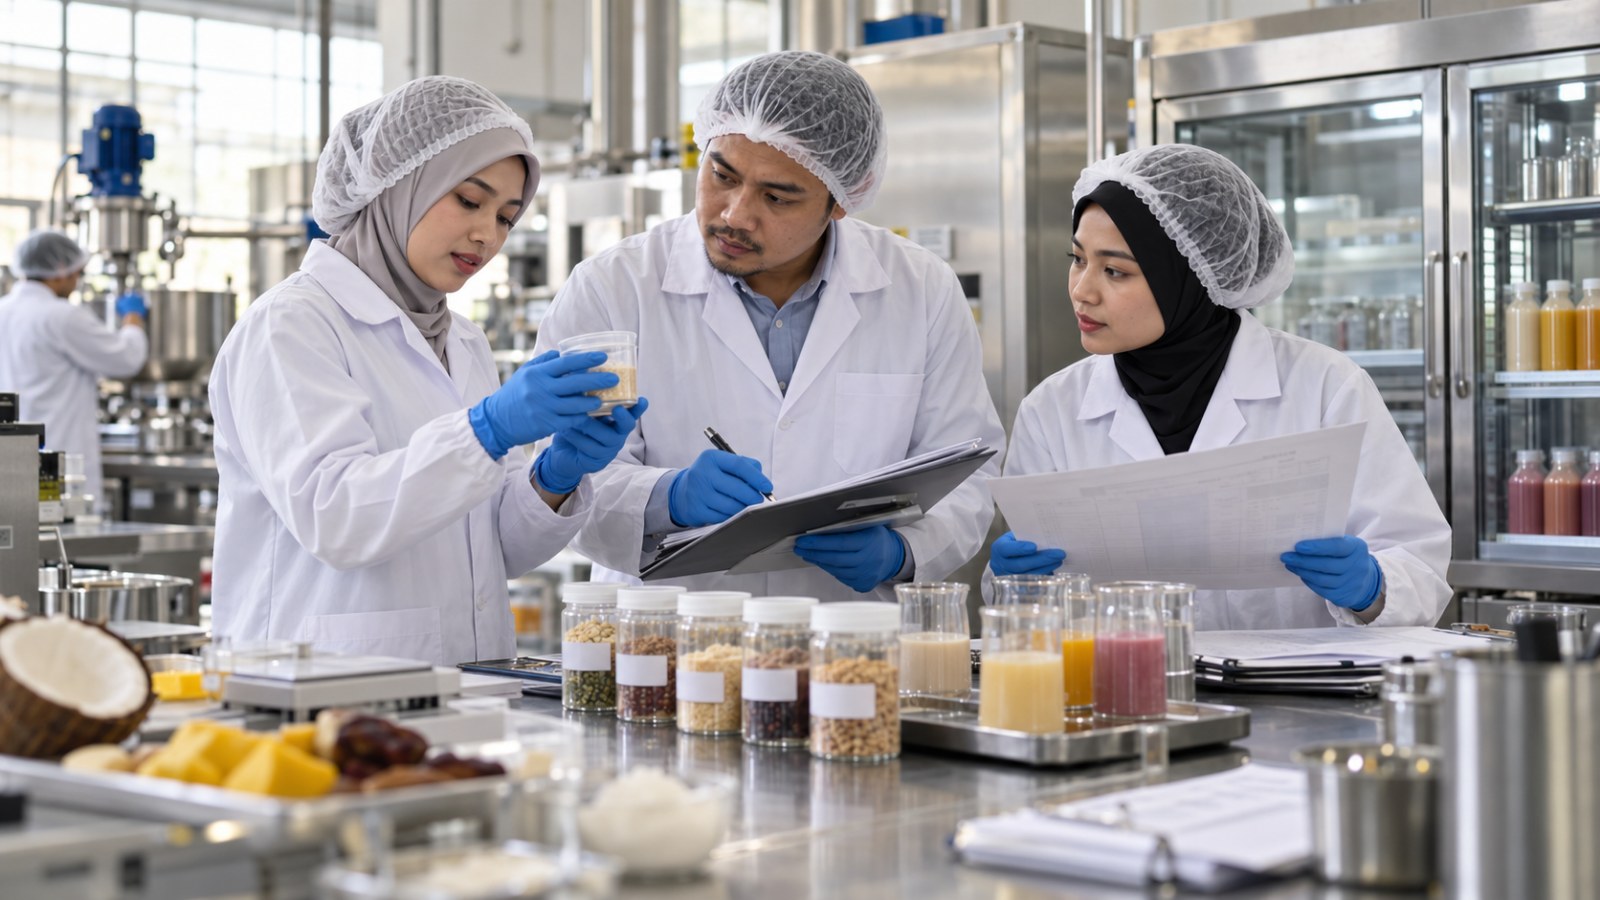
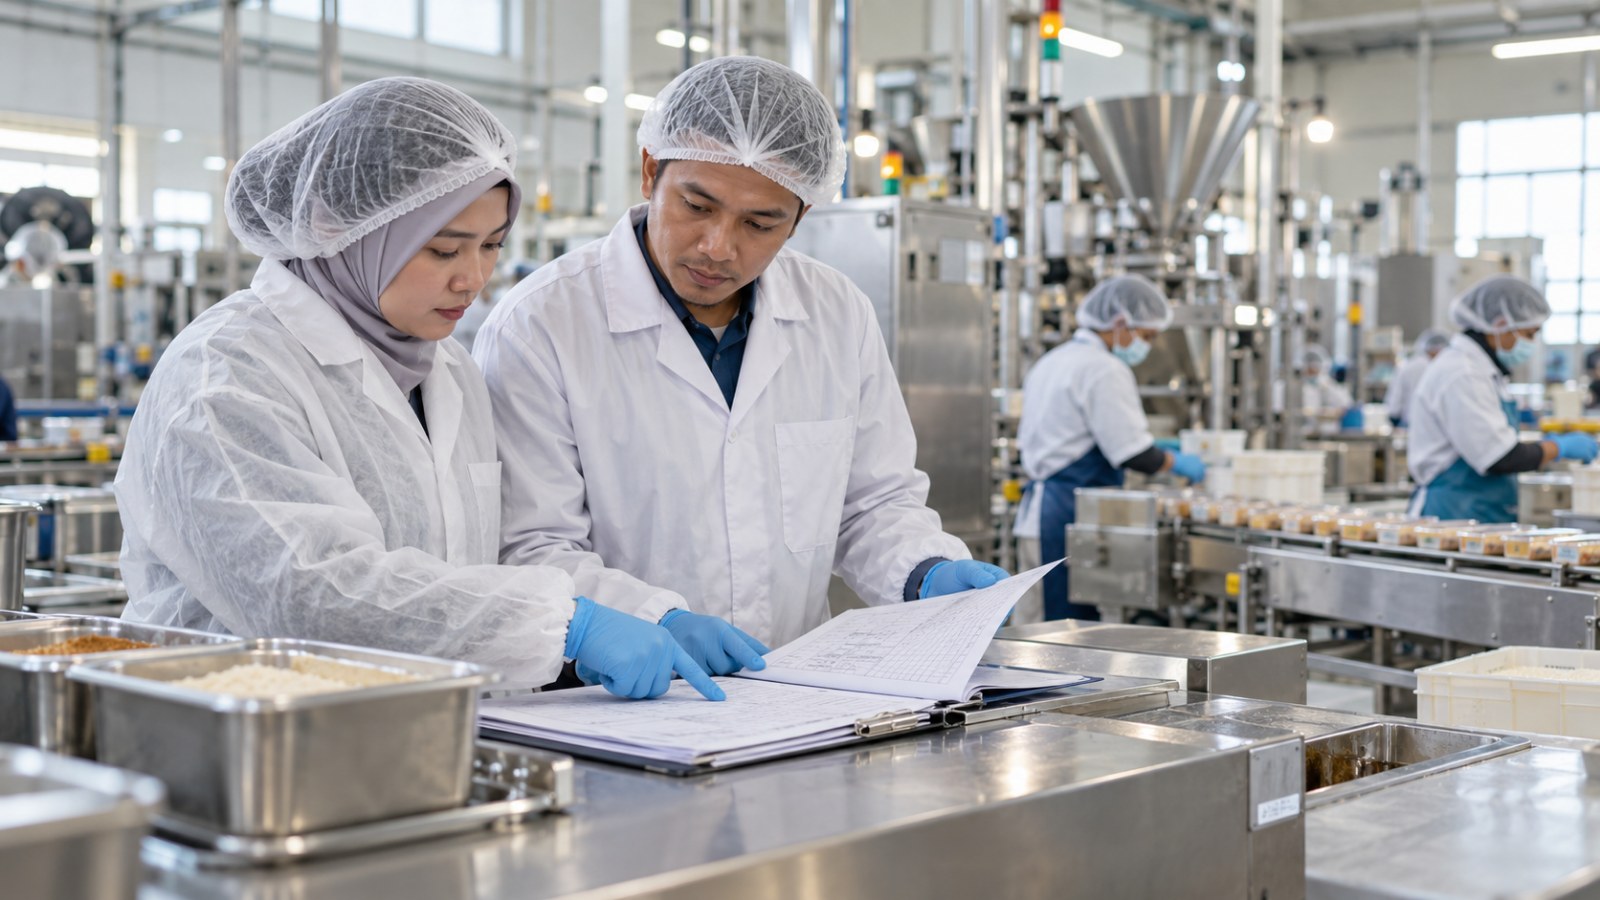
A halal food factory finishes its evening shift with several production batches completed, one ingredient delivery awaiting verification and a packaging machine that has not yet been released after maintenance.
The incoming team arrives. Production targets are waiting, warehouse employees are preparing materials and the next supervisor wants to start the first batch on schedule.
If the outgoing supervisor simply reports that “everything is fine”, important information may never reach the people making the next production decisions.
This is why a production shift handover should be more than a conversation about output quantities and machine availability.
For halal-certified food manufacturers, shift changes are operational control points where information about approved materials, product identity, equipment status, cleaning, segregation and unresolved deviations must pass accurately from one team to another.
A useful handover system does not need to be complicated. It needs to make unfinished decisions visible, identify who has authority to resolve them and prevent an unresolved issue from silently becoming normal production.
Why Shift Changes Create Halal Management Risks
Many factories operate with separate production, warehouse, quality assurance, maintenance and halal-management responsibilities.
During a single shift, employees may discover an ingredient discrepancy, isolate questionable stock, change a production schedule or begin equipment maintenance.
The employees who understand those events may leave before the next shift begins.
That creates a communication gap.
Common situations include:
- An incoming operator assumes a material is approved because it is already beside the production line.
- A quarantined ingredient is moved without the incoming warehouse team understanding its status.
- A cleaning activity is reported verbally but has no completed verification record.
- An unfinished batch is restarted without confirming the previous production conditions.
- An urgent production change is discussed between supervisors but has not passed the required review.
- A deviation is entered in a logbook without assigning responsibility for the next action.
None of these situations automatically establishes a halal certification breach. However, each represents a potential breakdown in operational control that deserves attention under the manufacturer’s applicable halal-management arrangements.
In Malaysia, the relevant framework includes the Malaysian Halal Certification Procedure, the Malaysian Halal Management System requirements and subsequent applicable amendments or circulars administered by the competent Malaysian halal authorities.
Businesses should apply the requirements relevant to their certification scheme and operation rather than assuming every factory follows an identical handover procedure.
Make the Handover About Production Status, Not Just Production Output
Traditional shift reports often focus on cartons produced, downtime, rejected products and outstanding orders.
Those figures are commercially important, but they do not tell the incoming supervisor whether production can safely and appropriately continue.
A stronger handover covers both performance and control status.
| Control Area | What the Incoming Shift Should Know | Useful Supporting Evidence |
|---|---|---|
| Raw materials | Which materials are approved, pending verification or restricted | Material status records and receiving information |
| Production batches | Which batches are completed, in progress, held or awaiting review | Batch records and production status |
| Equipment | Whether equipment is available, under maintenance or awaiting release | Maintenance and equipment release records |
| Cleaning | Which cleaning activities are completed and which require further checks | Cleaning records and applicable verification evidence |
| Segregation | Which materials or products must remain separated or restricted | Warehouse labels, location records and status identification |
| Deviations | Which problems remain open and who is responsible | Deviation reports and corrective-action records |
| Personnel | Who is authorised to make unresolved quality or halal-related decisions | Responsibility matrix and escalation contacts |
This table is an operational planning tool, not an official JAKIM form. Manufacturers should adapt it to their approved procedures, product risks, production arrangements and applicable certification conditions.
1. Transfer the Status of Every Unfinished Production Batch
A production batch does not become a new batch simply because the clock passes the shift-change time.
If manufacturing continues across shifts, the incoming team should understand exactly what has already happened.
Useful information includes:
- Product name and batch identification.
- Approved formulation or production instruction being followed.
- Raw materials already issued or consumed.
- Production stage reached at handover.
- Outstanding process checks or verifications.
- Any deviation affecting the batch.
- Whether continued processing has been authorised.
Consider a sauce manufacturer operating a mixing and filling process.
The outgoing team may complete mixing but leave the filling stage for the next shift. The incoming team needs more than a message saying that the sauce is ready.
It should be able to confirm the batch identity, process status, applicable holding conditions, recorded checks and whether any unresolved issue affects the decision to proceed.
Where food safety limits or critical controls apply, the relevant monitoring and release procedures must remain effective across the handover.
The objective is continuity of verified information, not simply continuity of machine operation.
2. Identify Restricted Materials Before the Incoming Team Uses Them
Ingredient verification is particularly vulnerable to communication problems when deliveries arrive close to a shift change.
For example, a warehouse may receive a raw material with an unexpected manufacturer name or an incomplete supporting document.
The receiving employee informs the outgoing supervisor and places the delivery aside.
Several hours later, the incoming production team sees the material near the staging area and assumes it is available.
A reliable handover should prevent this misunderstanding.
Restricted or unapproved materials should remain under the company’s established identification, segregation and release controls until the appropriate review is completed.
The handover should identify:
- The affected material and batch or lot.
- The reason its status is uncertain.
- Its current physical location.
- The department responsible for reviewing it.
- Any products or production orders that may be affected.
- The person authorised to communicate the release decision.
In Malaysia, material and supplier changes may also require action under the applicable halal certification procedure. An ordinary shift supervisor should not interpret an unexpected material as automatically approved merely because production needs it urgently.
The distinction between an existing approved ingredient and a proposed new source should be reviewed through the company’s established halal-management process.
3. Separate Equipment Availability From Equipment Release
A machine can be mechanically available without being ready for production.
Maintenance may have been completed while cleaning, inspection, process verification or another required activity remains unfinished.
That distinction matters when equipment is shared between production activities or when engineering work introduces materials that require assessment.
For example, a packaging machine may be returned by maintenance after replacing a component.
The incoming production team should establish whether the equipment has passed the relevant return-to-service controls rather than assuming that the absence of technicians means it is ready.
A practical equipment handover identifies:
- Equipment identification and location.
- Maintenance or cleaning work performed.
- Outstanding inspections or checks.
- Whether any materials used during maintenance require review.
- The current equipment status.
- The person or function authorised to approve production use.
Not every maintenance task creates a halal issue. The level of review should reflect the equipment, materials, process and risks involved.
Nevertheless, the incoming team should never have to guess whether a required release step has been completed.
4. Give Unresolved Deviations a Named Owner
A handover log can contain many entries and still fail if nobody is accountable for acting on them.
Consider an outgoing supervisor recording:
“Ingredient label different. Check tomorrow.”
The statement identifies a concern but leaves several questions unanswered.
Which ingredient? Which lot? Has the material been isolated? Who must check it? Can related production continue? What evidence is needed to close the issue?
A better handover converts observations into controlled actions.
A Practical Stop–Hold–Release Framework
| Status | Meaning | Expected Action |
|---|---|---|
| Stop | A condition requires the affected activity to cease under the established procedure | Prevent continuation and escalate to the responsible authority |
| Hold | The affected material, batch or equipment cannot yet be released | Maintain identification and control while verification continues |
| Release | Required reviews and approvals have been completed | Record the authorised decision before proceeding |
This is a suggested internal decision framework. It does not replace the manufacturer’s formal non-conformity, quarantine, product release or halal-management procedures.
Businesses should also avoid giving production supervisors authority that properly belongs to quality assurance, the halal function or another designated decision-maker.
5. Use a Short, Structured Handover Between Supervisors
A long report is not necessarily a better report.
In a busy factory, employees need a handover method that highlights exceptions without hiding them inside routine production figures.
One approach is to divide the discussion into three stages.
Stage One: Confirm the Current Situation
The outgoing supervisor identifies running batches, available equipment, active material restrictions and incomplete activities.
Stage Two: Review Exceptions
Both supervisors review any unresolved deviation, pending approval, maintenance restriction or production change.
The incoming supervisor should confirm where affected materials or equipment are located and which activities must not proceed.
Stage Three: Confirm Ownership
Every important open item receives a responsible person, required next action and an appropriate review point.
A brief acknowledgement by the incoming supervisor makes it easier to establish that the information was received.
Digital systems can support this process, but a well-controlled paper log may also be workable for a smaller manufacturer.
The important feature is not the technology. It is whether critical information remains visible and actionable.
6. Train Employees to Recognise What Must Be Escalated
Supervisors cannot hand over information they never receive.
Operators, warehouse employees, cleaners and maintenance personnel therefore need to understand which issues require immediate reporting.
Training can use realistic scenarios:
- An ingredient arrives under a manufacturer name different from the approved record.
- A cleaning verification is incomplete when the next team arrives.
- A production employee notices that an ingredient label does not match the batch instruction.
- Maintenance finishes work but the equipment release is not recorded.
- An urgent customer order requires an unplanned manufacturing change.
- A material intended for quarantine appears in the normal production staging area.
Employees should know how to protect the affected activity, who to contact and which decisions they are not authorised to make.
Training effectiveness can be checked through observation and short practical exercises rather than relying only on attendance records.
International food hygiene guidance under the Codex General Principles of Food Hygiene also emphasises appropriate personnel training, supervision and effective operational controls. These are complementary food safety principles, not substitutes for Malaysian halal certification requirements.
7. Review Handover Quality Using Measurable Indicators
Manufacturers can improve shift handovers by examining the problems that repeatedly cross shift boundaries.
Useful operational indicators include:
- Number of unresolved items carried into the next shift.
- Percentage of open items assigned to a responsible owner.
- Number of material-status misunderstandings found after handover.
- Cases where equipment use was attempted before required release.
- Repeat deviations associated with communication failures.
- Time taken to close higher-priority handover issues.
- Instances where the incoming team could not locate the supporting record.
These indicators should be interpreted carefully.
A factory reporting more deviations after introducing a better handover process may simply be identifying problems that previously went unreported.
The objective is not to reduce the number of reported issues at any cost. It is to improve visibility, timely escalation and effective resolution.
Management should also avoid using a handover completion target to pressure employees into signing off unresolved controls.
A Practical Shift Handover Checklist
Before accepting responsibility for the next production period, the incoming supervisor can use the following checklist as a starting point.
- Confirm production identity. Identify active products, batches, formulations and unfinished processing stages.
- Check material status. Establish which materials are available and which remain restricted, quarantined or under review.
- Review equipment readiness. Confirm the status of maintenance, cleaning and any required return-to-service approval.
- Identify open deviations. Review exceptions that may affect production decisions or product status.
- Check segregation arrangements. Confirm that restricted materials and products remain under appropriate control.
- Review planned changes. Identify substitutions, new processes or operational changes requiring approval.
- Assign unresolved actions. Make sure each significant issue has a responsible owner and next step.
- Confirm escalation contacts. Know who can authorise decisions involving quality, halal management or product release.
- Record the handover. Preserve an appropriate record of the information communicated and acknowledged.
- Verify before restarting. Do not assume the completion of a shift handover automatically releases a held material, batch or machine.
Factories should incorporate relevant parts of this checklist into their approved operating procedures rather than creating an unrelated parallel system.
Make the Handover Process Proportionate to the Factory
A small food manufacturer operating two shifts does not need the same reporting infrastructure as a large regional manufacturer with several production sites.
For a smaller operation, a controlled logbook, clearly identified material-status area and daily review of unresolved issues may provide a useful starting point.
A larger factory may benefit from an integrated production-management system connecting batch status, warehouse inventory, equipment maintenance, quality records and assigned actions.
In either case, the system should answer four questions without ambiguity:
- What is the current status?
- What remains unresolved?
- Who has decision-making authority?
- What evidence supports the decision to proceed?
If the system cannot answer these questions, more software or additional forms may simply create more records without improving control.
Reliable Production Records Can Support Wider Business Achievements
Consistent production handovers can also improve the reliability of a manufacturer’s operational data.
When batch quantities, production dates, equipment usage, output measurements and exceptions are recorded consistently, management is better positioned to evaluate genuine business performance.
A manufacturer may eventually document an exceptional measurable achievement involving production capability, product output or another clearly defined operational milestone.
If that achievement meets the relevant assessment criteria and can be supported by credible evidence, the business may separately consider applying for Asia Record recognition.
Such recognition concerns the measurable achievement. It does not establish halal status, confirm compliance with Malaysian halal certification requirements or replace approval from JAKIM or other competent halal authorities.
Production records are valuable first and foremost because they support reliable operations and accountable decision-making.
A Good Shift Handover Prevents the Next Shift From Inheriting Unknown Risks
The most important question at the end of a production shift is not only how much the factory produced.
It is whether the incoming team understands exactly what it is taking responsibility for.
Unfinished batches, restricted materials, equipment release conditions and unresolved deviations should not disappear when employees clock out.
A disciplined handover keeps those issues visible until the responsible people have reviewed and resolved them.
For halal food manufacturers, this strengthens the connection between documented halal-management arrangements and the decisions made on the factory floor.
The result is a more dependable operation where production continuity does not depend on assumptions, personal memory or informal messages between shifts.